Bags and luggage are among the highest-demand categories in export trade — rolling suitcases, backpacks, handbags, cosmetic bags, briefcases; virtually every manufacturing cluster produces them. Yet what truly costs buyers is rarely how good the sample photos look. It is whether the bulk production matches the approved sample, and whether the workmanship can stand up to everyday use. Third-party inspection is, in essence, verifying the production lot from the buyer’s side against the purchase contract, the specification sheet and the approved sample — checking workmanship defects, quantities, packaging, and more. Following a real inspector’s on-site workflow, this bag inspection guide walks through, step by step: what to check, how to check it, and how to judge what you find.
I. Common Bag Inspection Defects and Workmanship Failures
Stiff zippers, missing teeth, split zippers — the most frequent complaint for bags and luggage, and the most direct source of failure in everyday use. A sticking slider, misaligned teeth, or uneven fabric feed during sewing can all cause rough operation or even a zipper burst. To cut costs, factories may swap in lightweight zippers or a different brand — something the eye often cannot catch on the spot. Only repeated on-site opening and closing exposes the problem.
Sticky trolley handle, wobble, lock failure — telescoping-handle fatigue rarely shows up during sampling inspection, yet customers report that after only a few uses the handle wobbles, will not retract, or the push-button lock no longer holds. On site, inspectors run extend/retract tests and wobble checks to judge handle clearance, spring-back and lock reliability.
Load deformation and detached handles — handles snapping when the bag is packed full, case shells collapsing, noisy wheels — these are after-sales-service disaster zones. On site, hanging-load and lift tests confirm whether structural strength and seam integrity meet requirement.
Workmanship and style drift — stitch density, hardware placement, silhouette construction, colors — any deviation, however small, from the approved sample marks the lot as one to be handled with caution.
II. The Seven-Step On-Site Inspection Method
An inspection can be scheduled before shipment (pre-shipment inspection, PSI) or inserted mid-production as a during-production inspection (DUPRO). Once on site, the core task is simple: take the production goods, hold them up against the order and the approved sample, and work through the seven steps one by one:
Sample draw and count — draw a representative sample per AQL or the customer-specified level. First count the total cartons and total pieces, and verify that the style numbers match the order — preventing short shipments and mixed packing.
Carton mark verification — check the outer carton shipping marks: product name, style number, quantity, gross/net weight, orientation arrows, country of origin and carton dimensions — all against the order and packing documents.
Packaging check — verify the inner box, hang tags, polybags, desiccant, packing method and cushioning protection against the packing specification, preventing transit damage and packing errors.
Product style — compare with the approved sample and the tech pack: silhouette, color scheme, hardware style and left-right pairing, to confirm the goods match the sample.
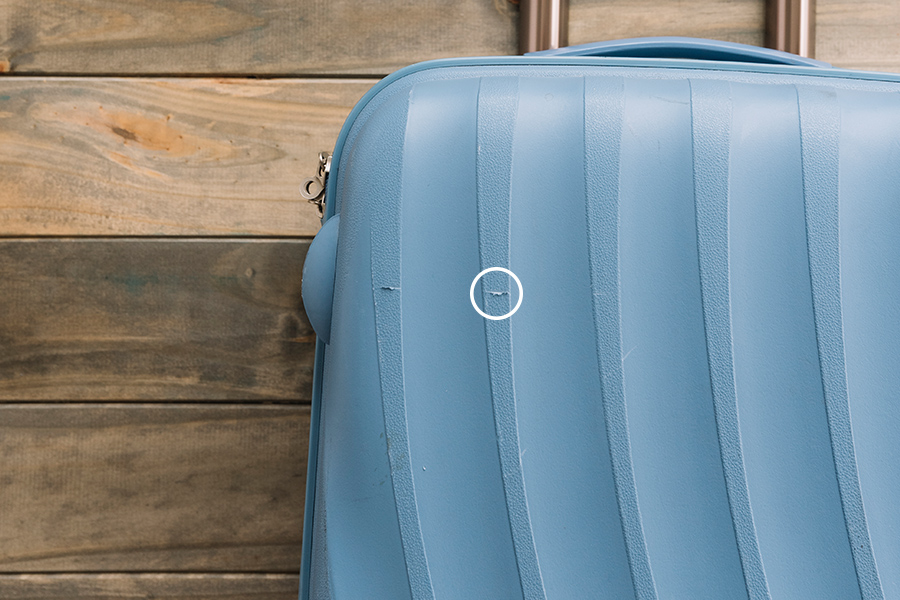
Appearance and workmanship — visually inspect for fabric flaws, skipped stitches, broken threads, glue overflow, stains and burrs on hardware. With gloves on, run hands along the edges to catch any sharp points that can cut.
Measurement — measure overall dimensions, capacity and hardware specifications with gauges and tape measures; check against tolerances to screen out out-of-spec dimensions and left-right asymmetry.
Testing — run on-site functional tests within the inspection scope: repeated zipper operation, trolley-handle extension and locking, hanging load for load-bearing capacity, wheel rolling and water-splash test. Record all measured results.
III. Quick-Reference Table of High-Frequency Bag Defects (Method / Tool / Classification)
| No. | Defect | On-Site Method | Tool | Classification |
|---|---|---|---|---|
| 1 | Stiff zipper / missing teeth / split zipper | Cycle the zipper 20–30 times; visually check tooth alignment and slider return; log even slight resistance | Visual / by hand | MAJ |
| 2 | Sticky trolley handle / wobble / lock failure | Extend and retract the handle 30–50 times; check locking and spring-back; judge wobble clearance by eye and feel | By hand / visual | MAJ |
| 3 | Load deformation / detached handle | Suspend the rated load and hold; repeatedly lift by the handles; watch for collapse, cracking, detachment | Load weights / visual | Detached handle = CR / Deformation = MAJ |
| 4 | Poor stitching / skipped stitches / broken threads | Visually check stitch-density uniformity; flex and pull the seam to check for stitch pull-out | Visual | MAJ |
| 5 | Fabric flaw / color shading / stains | Inspect under natural light plus a standard light source; compare color and feel against the approved sample | Visual | MIN / MAJ |
| 6 | Misaligned hardware / burrs / wrong logo | Visually check hardware position, burrs and engraving; verify against the approved sample | Visual | MAJ |
| 7 | Wrong or missing carton marks / hang tags / packing errors | Check the shipping marks carton by carton against the packing list and packing documents | Visual | MAJ |
| 8 | Wrong style / design mismatch (goods not conforming to sample) | Check silhouette, color scheme, hardware and left-right pairing against the approved sample | Visual | CR / MAJ |
| 9 | Sharp edges / rough edges that cut | Rub edges with gloved hands; inspect for burrs and sharp edges under light | By hand | CR |
| 10 | Wrong dimensions / capacity | Measure dimensions and capacity with gauges and tape measures; screen against tolerances | Gauge / tape measure | MAJ |
IV. Inspection Priorities by Product Category
| Category | Key Risks | On-Site Focus |
|---|---|---|
| Rolling suitcases / luggage | Trolley-handle fatigue, wheel noise, case load-bearing capacity | Handle extension & locking, hanging-load test, rolling test |
| Backpacks / daypacks | Shoulder-strap attachment, zipper smoothness, capacity deviation | Lift test on stitching, zipper operation test, dimension measurement |
| Handbags / cosmetic bags | Hardware burrs, lining quality, silhouette distortion | Hardware visual check, appearance workmanship, sample comparison |
V. AQL Sampling and Lot Acceptance — Quick Reference
Sample sizes follow AQL, General Inspection Level II (ANSI/ASQ Z1.4 / ISO 2859-1): 500 pcs → sample 50; 1,000 → 80; 3,200 → 125; 10,000 → 200. Critical (CR) defects: AQL 0 — a single finding rejects the lot. Major (MAJ): AQL 2.5. Minor (MIN): AQL 4.0. Exact accept/reject numbers are read from the standard tables; here we provide sample-size baselines only.
VI. Pricing and Standard Process
Book online, specifying the product, quantity, inspection location and preferred date.
The inspector performs on-site verification, recording defects and measured data.
A formal report with the AQL judgment and photos can be issued the same day.
For rejected lots, we assist with negotiating rework or sorting with the factory.
Pricing: starting from CNY 600 per person-day (overseas clients are billed in USD). Orders are scheduled the same day, inspections are completed the next day, and reports are issued within 4 hours of inspection — the entire process takes as little as 2 calendar days.
VII. Frequently Asked Questions
Q1: How many pieces are sampled in a bag inspection?
Following AQL, General Inspection Level II (ANSI/ASQ Z1.4 / ISO 2859-1): 500 pcs → sample 50; 1,000 → 80; 3,200 → 125; 10,000 → 200. AQL levels: CR 0, MAJ 2.5, MIN 4.0.
Q2: Can zippers and trolley handles be judged on site?
Yes. Repeated opening and closing reveals sticking and zipper splits; extend and retract the trolley handle 30–50 times and check locking and wobble. Obvious jamming, failure to retract, or a lock that will not hold is classified as MAJ.
Q3: How is load-bearing capacity tested?
On site, suspend a rated load and hold, then repeatedly lift by the handles, watching for case-shell collapse, cracking and handle detachment. A detached handle is CR; significant deformation is MAJ.
Q4: What is the difference between inspection and testing?
Inspection verifies, on site, whether this particular lot matches the contract, the specification sheet and the approved sample. Material composition, chemical safety and regulatory performance belong to laboratory testing. The two complement each other — neither replaces the other.
Q5: What does “goods not conforming to sample” mean?
The bulk production’s silhouette, color scheme, hardware or dimensions differ from the approved sample. This is a core check item during inspection, and serious discrepancies are classified CR/MAJ.
Q6: How much does inspection cost, and how quickly?
Starting from CNY 600 per person-day (overseas clients billed in USD). Orders are scheduled the same day, inspections are completed the next day, reports are issued within 4 hours of inspection, and everything can be done in as little as 2 calendar days.